


















Lesson 27 of 49 · Machining
Chapter review: machining
Review the machining chapter: a one-picture summary, a recap table of formulas, a speed-and-power planner you can run, and a ten-question mixed quiz.
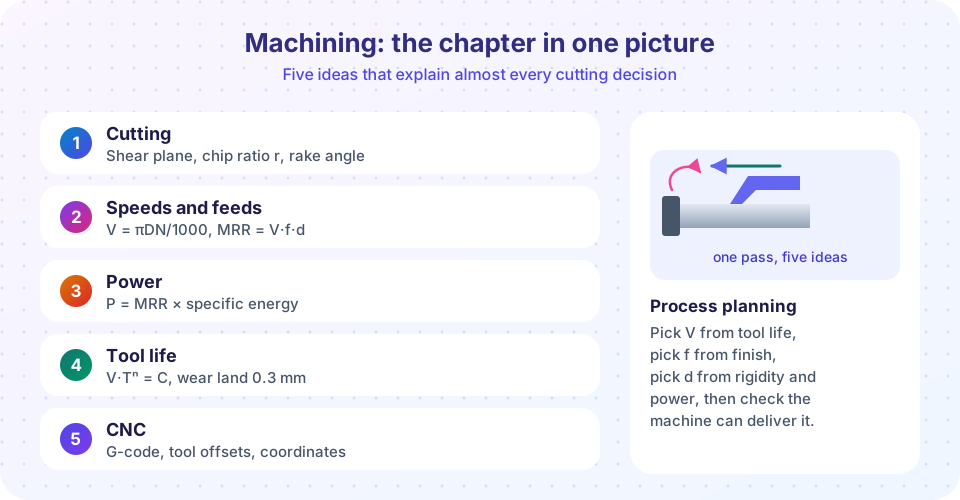
You have now followed a cut from the first contact of the tool to the cost of a finished part. This review ties the pieces together. Read the picture, scan the table, try the planner on your own numbers, and then test yourself with the quiz at the end. If any answer surprises you, the table tells you which lesson to reread.
What you will learn
- How the five ideas of the chapter fit into one planning routine.
- Which formula to reach for in each situation.
- How to check a planned cut against machine power.
Key terms
Process plan: the ordered list of operations, tools, speeds and feeds for making a part.
Roughing and finishing: a fast pass with large feed and depth that removes bulk, then a light pass for size and surface.
Power limit: the cut that the spindle motor can drive without stalling; often the first limit you hit in roughing.
Recap table
| Idea | Key equations | Rule of thumb |
|---|---|---|
| Chip formation | r = t0/tc = sin φ / cos(φ − α), γ = cot φ + tan(φ − α) |
Positive rake and low friction give a bigger shear angle |
| Forces | F = Fc sin α + Ft cos α, N = Fc cos α − Ft sin α |
Thrust force does no work but bends the tool |
| Speed | V = π D N / 1000 |
V comes from tool and work material, N follows |
| Removal rate | Turning V f d × 1000; milling ae ap vf |
Depth of cut costs the least tool life |
| Power | P = MRR × u |
Divide by drive efficiency for the motor |
| Finish | Ra ≈ f² / (32 r) |
Small feed and big nose radius |
| Tool life | V Tⁿ = C |
A 20% speed rise can halve carbide life |
| Cost | T_opt = (1/n − 1)(tc + Ct/Cm) |
The cheapest speed is neither the fastest nor the slowest |
| CNC | G00, G01, G02/G03, G54, G43 | Offsets connect the program to reality |
A planning routine
- Choose a tool material and grade for the work material and the cut type (smooth or interrupted).
- Pick V from the tool maker's range, adjusted by the tool life you want.
- Pick feed f from the finish required: large for roughing, small for finishing.
- Pick depth d from the stock allowance and the machine's rigidity.
- Calculate N, MRR, power and time. If the power exceeds the machine's rating, reduce depth first (it affects tool life least), then feed.
- Write the program, run the first part slowly, measure, and apply offsets.
Common misconceptions
"The settings in the catalog are the answer." They are a starting point. The actual best values depend on rigidity, coolant, the batch size and the tool cost.
"If the power is enough, the cut is fine." Rigidity and chatter (self-excited vibration) can limit a cut long before power does, especially with long tools and thin walls.
Try it
Here is a short planner that checks a turning cut against a machine's power. Change the inputs and watch which limit you hit.
Press Run (or Ctrl + Enter) to see the result here.
Program input · what you'd type while the program runs
Type the answers before you press Run, one per line. Each time the program reads a line (with input()), it gets the next line from this box.
Then a quick drill for the rpm formula. It makes up a diameter and a cutting speed; you give the spindle speed.
Check your understanding
Quick check · 10 questions
of 10 answered You scored / 10 · perfect!
-
1. A chip is 0.30 mm thick from a 0.15 mm uncut layer. What is the chip thickness ratio?
r = t0 / tc = 0.15 / 0.30 = 0.5. -
2. Which force is multiplied by cutting speed to give cutting power?
Only the cutting force acts along the direction of motion, so P = Fc × V. -
3. What is the spindle speed for a 25 mm cutter at 100 m/min?
N = 1000 × 100 / (π × 25) = 1,273 rpm. -
4. Removal rate in turning with V = 200 m/min, f = 0.25 mm and d = 2 mm is:
200 × 0.25 × 2 × 1000 = 100,000 mm³/min = 100 cm³/min. -
5. A finishing pass is changed from f = 0.2 mm to f = 0.1 mm. The ideal Ra becomes:
Ra is proportional to f squared, so halving the feed divides it by four. -
6. If the machine is power limited, which setting should you reduce first to keep tool life?
Depth of cut raises force and power but changes tool life much less than speed does, so it is the first setting to trade. -
7. Which tool material would you choose for aluminum with a long life?
PCD resists the abrasive silicon in aluminum alloys and does not react with aluminum, so it lasts very long. -
8. In Taylor's equation with n = 0.2, what happens to tool life if you cut 10 percent slower?
T scales as V^(-1/n) = V^(-5). At 0.9 V: 0.9^(-5) = 1.69, an increase of about 69 percent. Life is very sensitive to speed. -
9. Which G-code line is a straight move at feed rate?
G01 is linear interpolation at the feed rate F. G00 is a rapid move and G02 is a clockwise arc. -
10. A tool at 100 m/min lasts 60 min and at 140 m/min lasts 20 min. Roughly what is n?
n = ln(140/100) / ln(60/20) = 0.336 / 1.099 ≈ 0.31.
Summary
- Chip formation is shear on a plane; rake angle and friction decide the shear angle and the force.
- Speed, feed and depth give rpm, removal rate, time, power and finish; check power and rigidity before you commit.
- Tool life falls steeply with speed (Taylor), so the cheapest speed lies between the slowest and the fastest.
- CNC programs move the tool; offsets connect the program to the real part.
Track your progress
Create a free account to tick off lessons and pick up where you left off on any device.
of Manufacturing Processes lessons completed